
A metal sheet can look flat when it arrives at the workshop and change shape after cutting. Another part may sit correctly in a fixture but twist as soon as the clamps are released. These changes can make bending, welding and assembly more difficult, increasing adjustment time and rework.
Sheet metal warping occurs when a sheet or cut component loses its intended flat shape. Understanding when the distortion develops is the first step toward correcting it. TFON’s approach to sheet and plate processing connects the condition of the incoming material with the requirements of the next operation.
Why Does Sheet Metal Lose Its Flatness?
Distortion rarely has a single explanation. Material history, heat input, part geometry and handling conditions can all influence the final shape.
Residual Stresses in the Material
Residual stresses remain inside a material even when no external force is applied. They can develop during manufacturing operations such as rolling, cooling and forming.
A sheet may appear flat while these stresses are balanced. Cutting the sheet changes its geometry and can redistribute that balance, allowing individual parts to bow or twist. This explains why components cut from the same sheet may behave differently depending on their shape and position.
Long, narrow parts and components with large cutouts can be particularly sensitive to changes in stress distribution.
Uneven Heating During Cutting and Welding
Thermal processes heat specific areas while the surrounding material remains cooler. The heated region expands and then contracts as it cools. When this movement is restrained by adjacent material, permanent deformation can occur.
Laser and plasma cutting can introduce local thermal effects alongside the release of existing stresses. During welding, uneven heating and shrinkage can produce angular distortion, bowing or twisting.
The result depends on material properties, thickness, geometry, heat distribution and restraint. Increasing machine power or changing cutting speed alone is therefore not a universal solution.
Coil Set and Existing Flatness Defects
Some shape defects exist before fabrication begins. Material supplied from a coil may retain longitudinal curvature after uncoiling. Sheets can also exhibit edge waves or waviness through the centre.
These conditions should be identified during incoming inspection. Otherwise, operators may spend time adjusting downstream equipment to compensate for a problem already present in the material.
Handling and Mechanical Loads
Inadequate support during lifting, storage or processing can bend thin sheets. Excessive clamping force may also temporarily pull a distorted part into position, hiding its natural shape until it is released.
Damaged supports, uneven loading and local impacts can introduce additional deformation. A reliable investigation should therefore include material handling as well as cutting and welding.
How to Identify the Cause of Sheet Metal Warping
Start by establishing when the shape changes. Compare the material before cutting, after cutting and cooling, after edge preparation, and after welding where applicable.
Measure parts using a suitable reference surface and inspection method. Check them in the support condition specified by the drawing or inspection procedure. A component held flat by a fixture does not necessarily meet its flatness requirement when released.
Useful information to record includes:
Material grade, thickness and batch.
Part dimensions, cutouts and narrow sections.
Cutting method and processing sequence.
The location and direction of the distortion.
Flatness measurements before and after each relevant operation.
This comparison helps distinguish an incoming material defect from deformation introduced later in production.
How to Flatten Warped Sheet Metal
Warped sheet metal is flattened by bending it past its yield point in a controlled way, so the stressed areas even out and the part stays flat once it is released. For sheet, plate and cut parts in production, this is done on a roller leveler. Single parts and local bends can be corrected on a press. Flame straightening, which uses local heating and cooling, is a separate method used mainly on welded structures.
The appropriate correction method depends on the material, geometry, severity of the defect and required tolerance.
Precision Roller Leveling
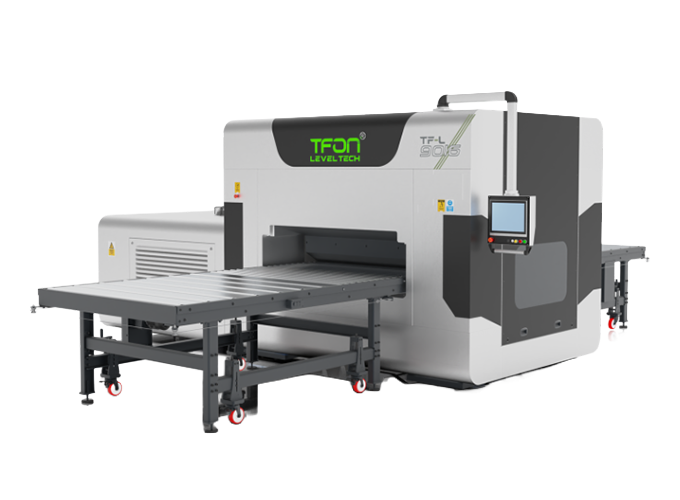
Roller leveling passes a suitable sheet or component through a series of alternating bends. With correctly selected equipment and settings, this process can improve flatness and redistribute residual stresses.
Machine suitability depends on factors including material strength, thickness, width and part geometry. Leveling should not be described as removing every internal stress or guaranteeing that a component will remain unchanged after subsequent operations.
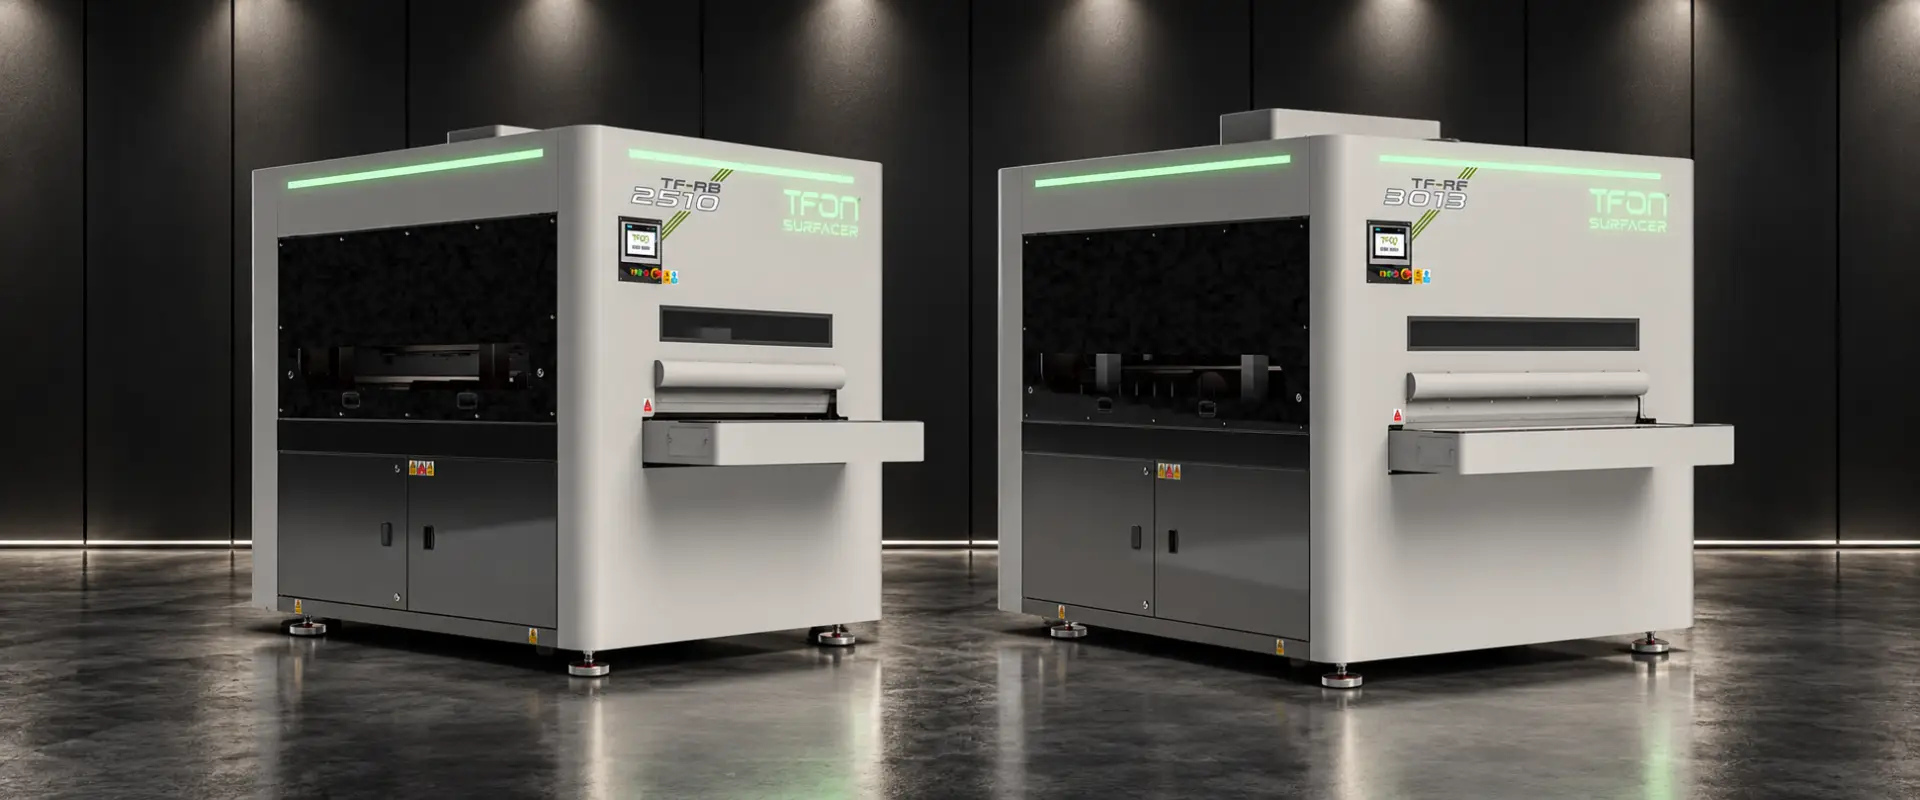
TFON Leveltech® sheet metal leveling machines are designed to improve the flatness of sheets, plates and cut parts from 0.3 to 30 mm thick before further processing; how roller leveling works explains the principle. Representative part trials help establish an appropriate setup and verify the achievable result.
To match a leveler to your thickness and width range, see the sheet metal leveler buying guide.
Local Mechanical Straightening
For certain components, controlled press straightening can correct local deformation. The process requires suitable supports, carefully applied force and repeated measurement.
Uncontrolled bending or hammering can leave surface marks and introduce new defects. The correction method should preserve critical dimensions and the component’s intended function.
Thermal Treatment Where Appropriate
Some applications require an engineered thermal stress-relief process. Its suitability depends on the alloy, material condition and production requirements.
Thermal treatment and mechanical leveling serve different purposes. A heat-treatment cycle should not be assumed to restore flatness automatically, and any dimensional changes must be checked afterward.
Where Edge Preparation Fits into the Process
Once a part meets the required flatness, the next operation may be preparing its edges for welding. Stable positioning and consistent bevel geometry help make this stage more repeatable.
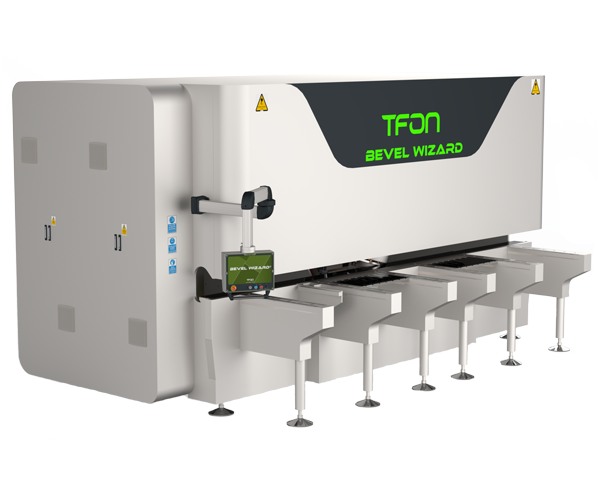
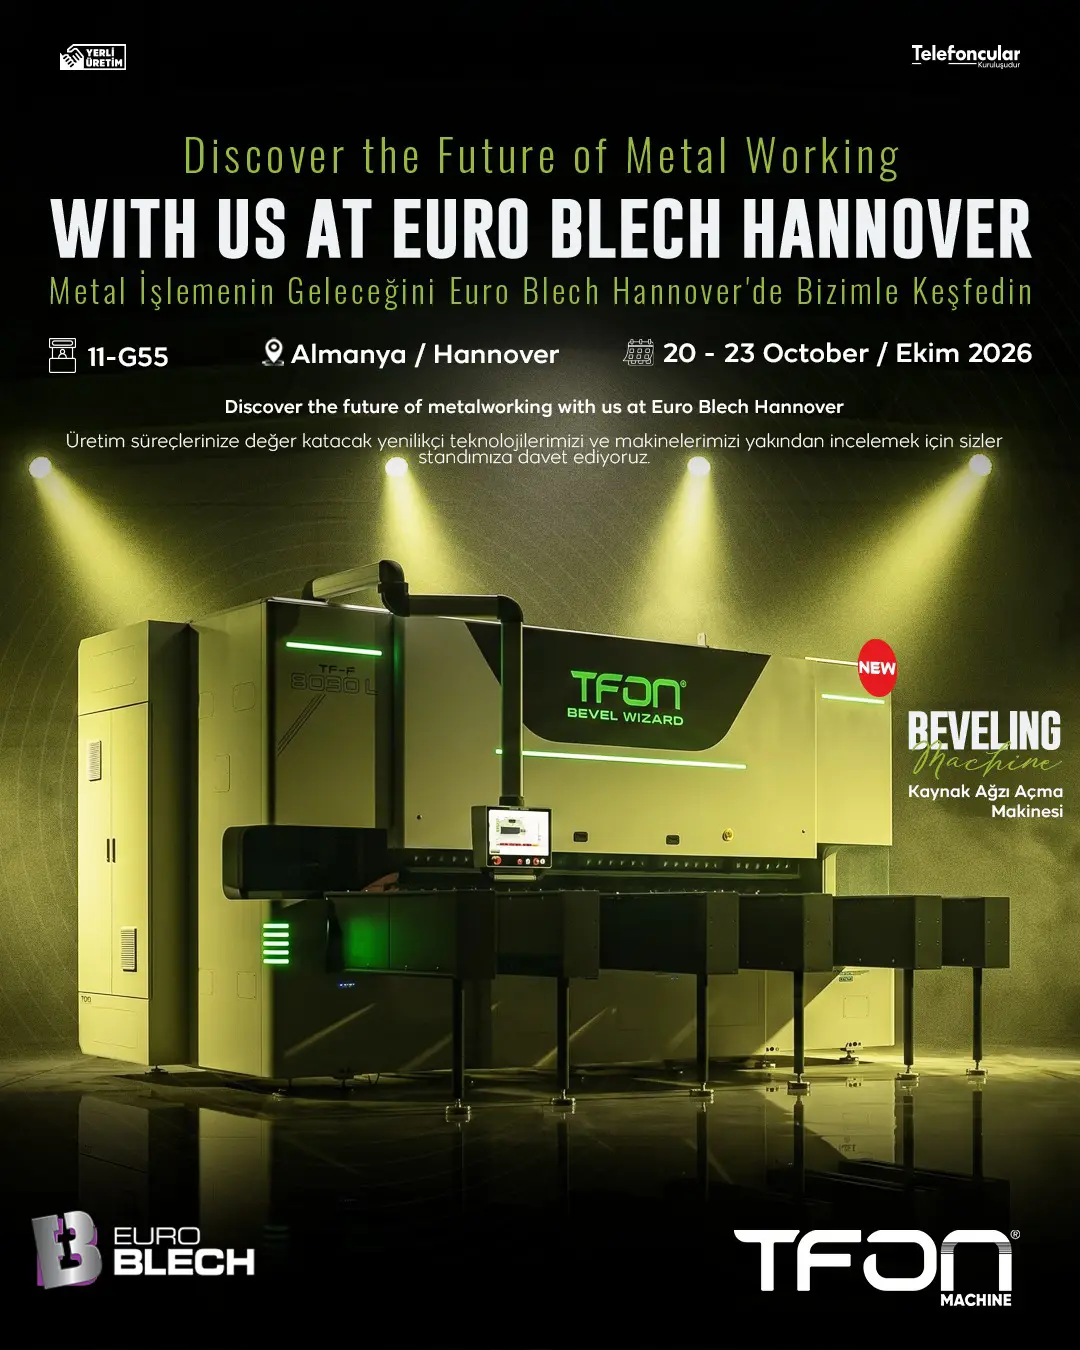
For suitable straight-edge applications, the TFON Bevel Wizard® TF-F 8030 L uses a fixed-table arrangement: the workpiece is mechanically secured while a moving abrasive unit performs the beveling operation. The product specifications list a material thickness range of 4–100 mm and a maximum processing length of 3,000 mm.
Its role is controlled weld preparation. Flatness correction must be addressed separately when the incoming part is distorted. Bevel angle, root face and other joint details should follow the applicable drawing and welding procedure.
This distinction matters because accurate edge preparation supports consistent fit-up, while welding sequence and heat control remain necessary to manage subsequent distortion.
How to Reduce Sheet Metal Warping
Reducing sheet metal warping requires attention to the complete production route. Inspect incoming material, support parts correctly and check flatness at stages where stress redistribution or heat input may change the shape.
Start with flat, low-stress material. Sheet that has been leveled before cutting releases less stress when parts are cut from it. Check incoming sheet for coil set and edge waves.
Nest and sequence cuts to spread heat. A cutting order that moves around the sheet, and enough web between parts to keep the skeleton stiff, limit local heat build-up. Small tabs or micro-joints can hold parts in place until cutting is finished.
Keep weld volume down. A correctly sized bevel needs less filler metal and fewer passes, which means less shrinkage. See how bevel angle affects weld quality.
Balance and sequence the welds. Weld on alternate sides of the neutral axis, use back-step or skip sequences on long seams, and use intermittent welds where the drawing allows.
Restrain or preset the part. Fixtures, clamps and presetting the parts slightly against the expected pull reduce final distortion. Measure after release, because a clamped part can hide its real shape.
Record successful settings and repeat measurements when material batches, part geometries or processing conditions change. If parts are still out of tolerance, flatten them on a roller leveling machine before the next operation.
Build the Correction Plan Around the Actual Part
Controlling sheet metal warping starts with identifying its cause and confirming the result of each corrective step. A process that works for one material thickness or geometry may need adjustment for another.
To assess the appropriate production sequence with TFON, prepare a drawing or sample part together with material details, current flatness measurements and downstream requirements. This provides a practical basis for coordinating leveling, edge preparation and subsequent fabrication while reducing avoidable rework.